$3M International Bridge Painting Project

Posted on Leave a comment

$3M International Bridge Painting Project Begins

MONDAY, JULY 18, 2022


Last week, a painting project to coat the Canadian side of the Sault Ste. Marie International Bridge began, using a one-coat paint system.

The steel truss arch bridge spans the St. Mary’s River between Sault Ste. Marie, Michigan, and Sault Ste. Marie, Ontario, and is the only vehicular crossing between those locations within a 300-mile distance. The structure is also the largest trade crossing in Northwestern Ontario, playing a “vital role” for both Soo communities, according to the bridge’s website.

Latest Coating Work

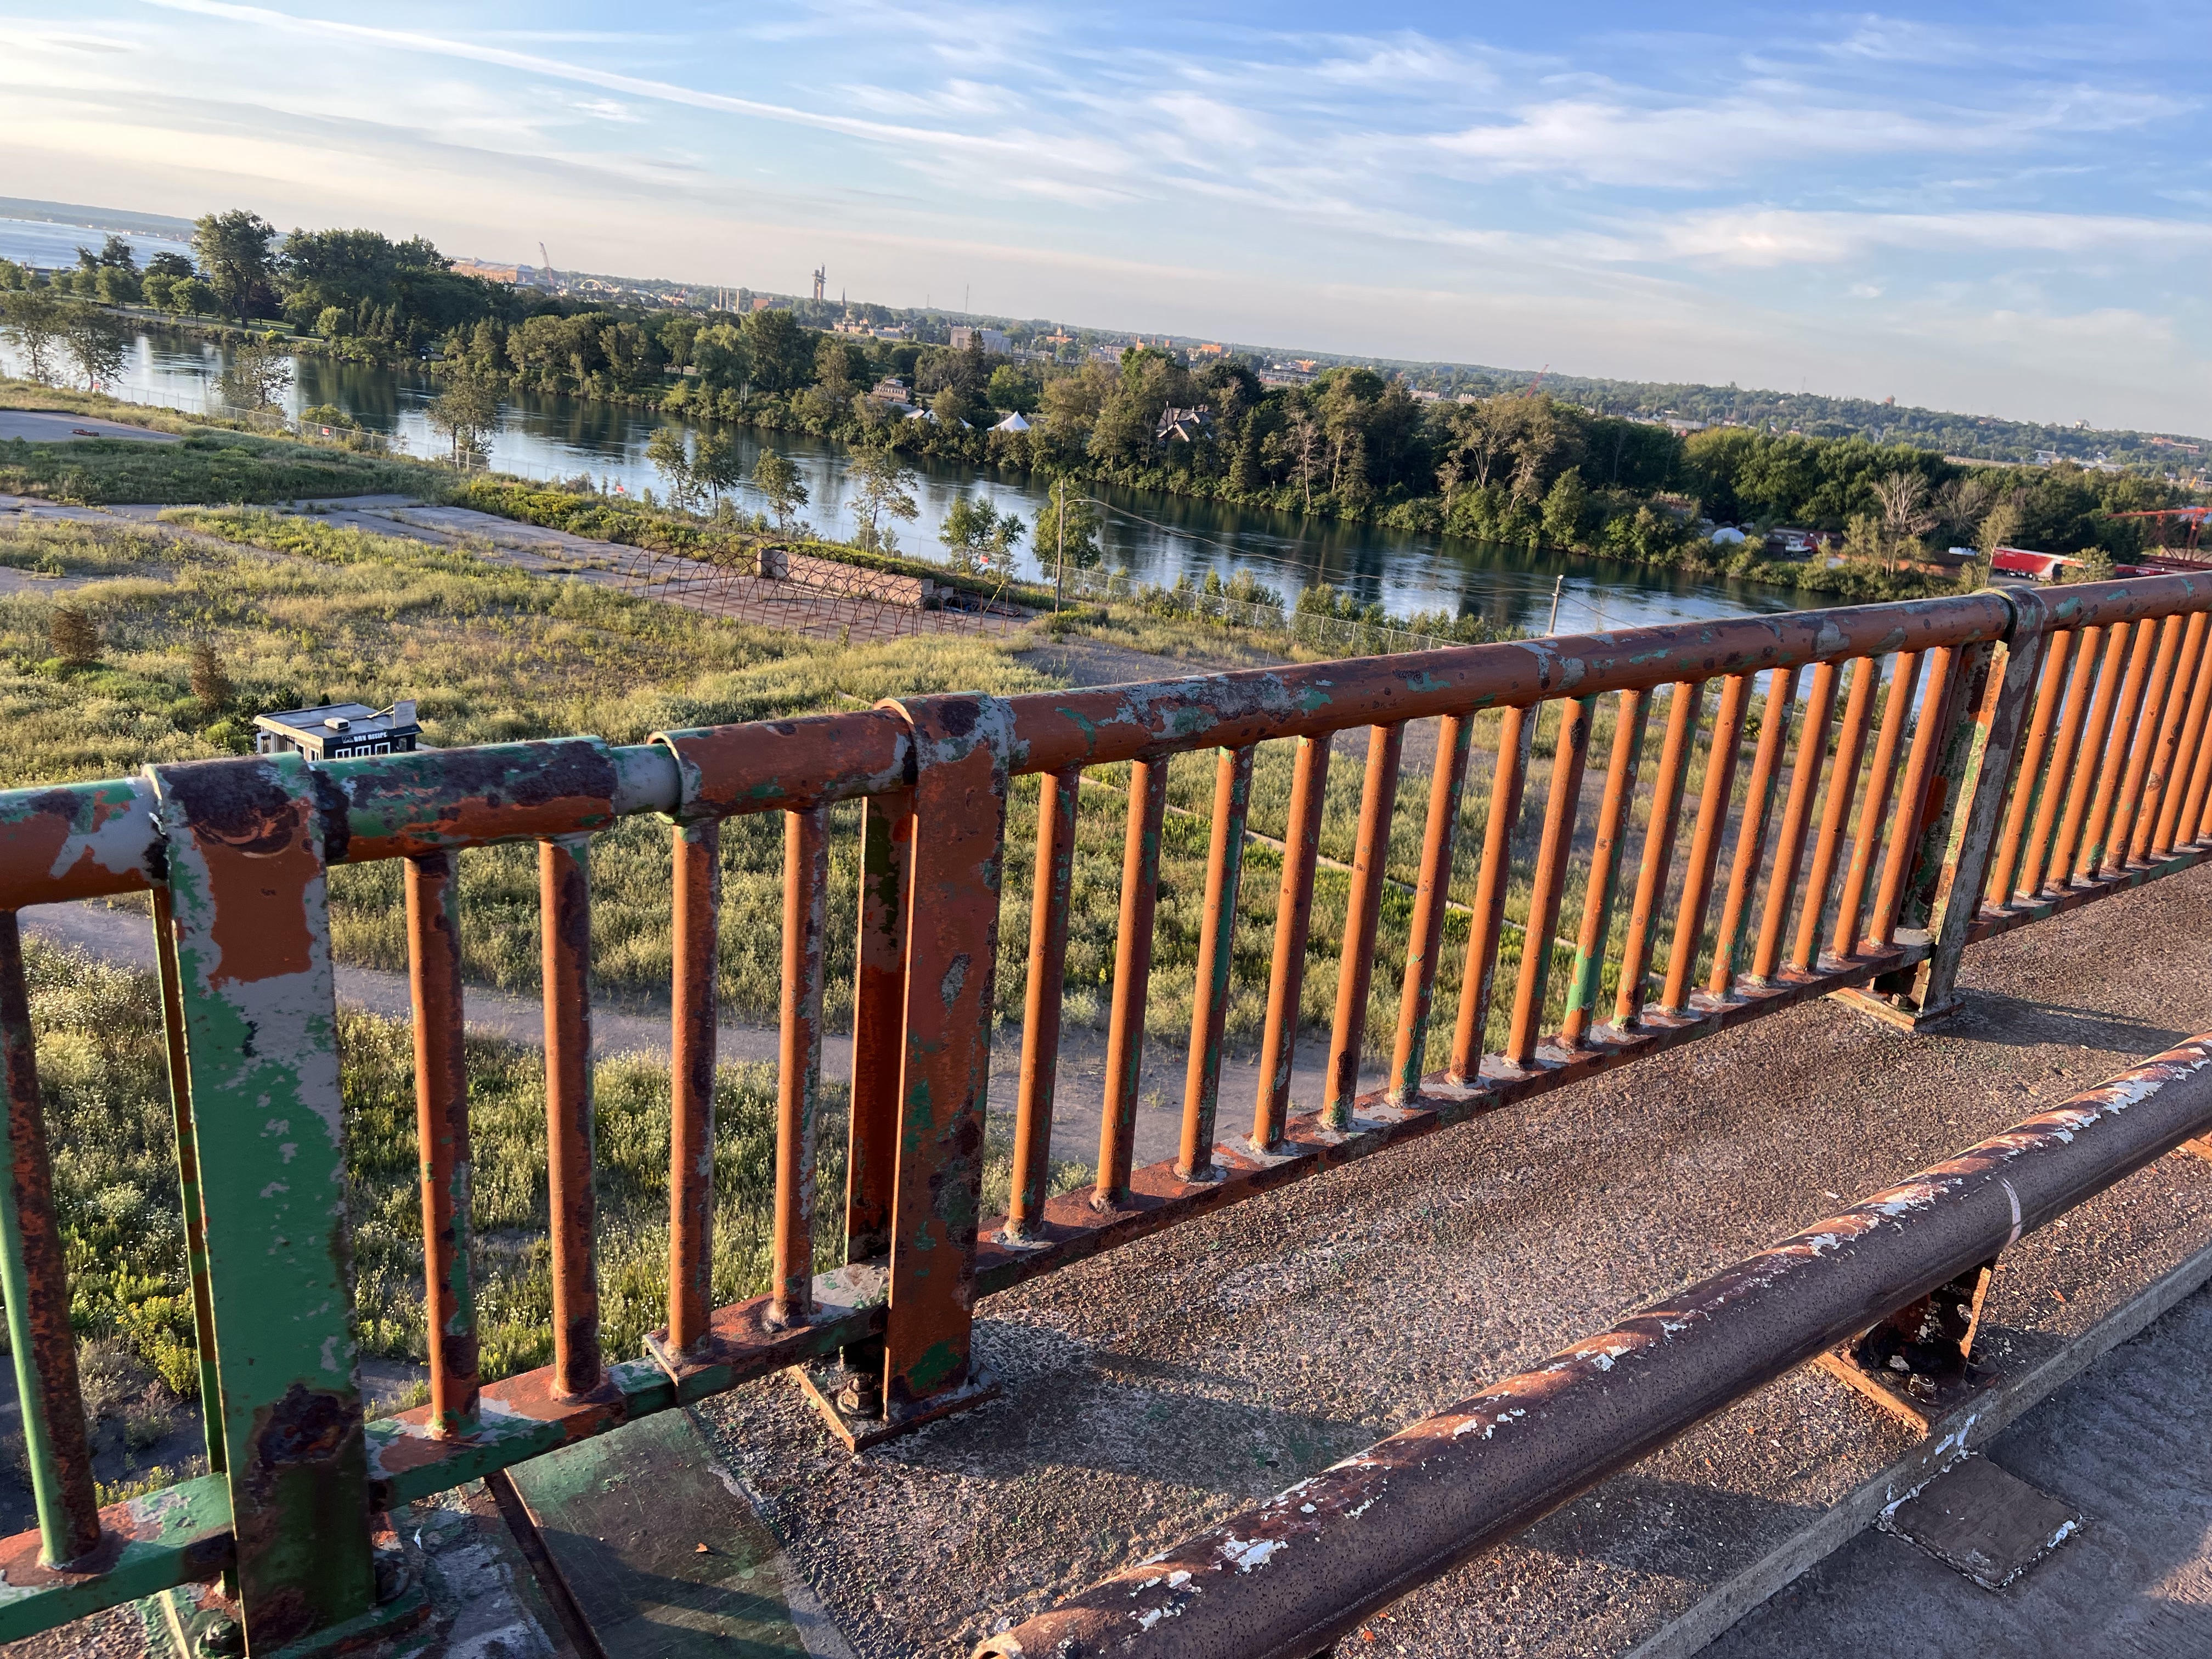
The $3 million painting project will coat the curb and service walk railing on the Canadian half of the bridge. Work is being completed by prime contractor source: https://www.paintsquare.com/news/view/?25293

For the coatings, the contractor will use a high-ratio calcium sulfonate alkyd (HRCSA) one-coat paint system.

“This innovative product and process offers many benefits,” said Bridge Engineer Karl Hansen. “We anticipate cost savings, enhanced corrosion resistance, quicker completion time, and minimized disturbance to the environment and our customers.”

US Army Corps of Engineers, Richard McDonald, public domain, via Wikimedia Commons
Last week, a painting project to coat the Canadian side of the Sault Ste. Marie International Bridge began, using a one-coat paint system.
Sault Ste. Marie International Bridge

According to the release, painting operations will be conducted at various locations around the Canadian side using moveable scaffolding. One lane of alternating traffic will be maintained during the painting.

“The International Bridge Administration (IBA) advises motorists to expect delays, remain alert for workers, and use caution when traveling through the work zone,” writes the IBA.

The project is fully funded through the Federal Bridge Corp. Limited with the help of a capital budget allocation approved by the Government of Canada. Work is expected to be completed by Nov. 1.

Previous Bridge Work

(Post-Interview video with contractor Matt Glavin, http://www.glavin.net, regarding his personal experience of working with HRCSA on the Canadian side of the Sault Ste. Marie bridge arch.)

HRCSA is Chemically Active

Posted on

When the word “Coating” is used, most people think of a paint that forms into a solid barrier film.

The HRCSA Self-Priming Topcoat is an unconventional coating system which is both chemically active and elastomeric.

Traditional barrier or sacrificial barriers cure across the steel micro voids leaving areas of exposed steel between the coating and the substrate – these micro void areas are vulnerable to rapid undercutting once the barrier is breached.

Typical causes of newly applied coating breaches: Workers walking on fresh coating during construction and take-down. Mechanical damage (tools being dropped), stone chips, debris, etc.

HRCSA is a reacted calcium sulfonate, calcium carbonate based complex that fully wets the surface as it neutralizes acids, displaces moisture and scavenges oxygen leaving no micro voids unfilled.

The high ratio of active calcium sulfonate thoroughly wets the micro voids creating a mono-molecular layer of cations which ensure chemical neutrality and no undercutting if the coating is breached. ( The HRCSA reacted formulation’s uniqueness is what gives it this performance advantage.) <Link to Specifications>

The role and function of HRCSA calcite platelets.

Once applied, the formulation’s artificially grown calcite crystals line up like fish scales to form a strengthened film with extended pathways for moisture and oxygen.

When acidic moisture (acid rain) passes through these crystals, a minute amount of the calcite dissolves to create a neutral base liquid void of acidity at the steel substrate.

Summarily, it neutralizes acids, displaces moisture, and scavenges oxygen.

HRCSA Penetrant/Sealer + HRCSA Self Priming Topcoat = Meld

When the word “Penetrant” is used, most people think of a low molecular weight epoxy or moisture cured urethane penetrants which were primarily designed to bind up existing rust on steel surfaces and a tiecoat.

Low molecular weight penetrants applied into active corroded connections do not chemically neutralize the active corrosion. Because they are epoxies or MCUs, they harden and then crack whenever movement occurs.
This explains why rust bleeding from connections can usually be seen < 2 years after application – the corrosion was never stopped.

HRCSA meld coat is both chemically active AND flexible.

Crevice corroded and pack-rusted joints and connections that are properly prepared (flushed, salt mitigated and dried) then pressure filled to refusal with HRCSA Penetrant-Sealer, Meld-coated with HRCSA self-priming topcoat and overcoated with same (wet on wet), creates a chemically active, flexible seal that actively stops corrosion inside the connection for years (even decades) to come.

Because the chemistry stays active in the connection allowing the structure to move without damaging the film.

HRCSA can applied by spray, brush or roller to anything Fe – including: steel of any type, as well as overcoating tightly adhered, contaminant-free existing coatings.

Pressure-Applying HRCSA Penetrant into flushed out, blown dried, cleaned corroded crevices before application of the HRCSA meld-coat.

Pack-rusted connections saturated with HRCSA Penetrant.

Application of HRCSA meld coat (thick layer of HRCSA self-priming topcoat overtop HRCSA Penetrant).

Same pack-rusted connection filled with HRCSA self-priming topcoat over top of HRCSA Penetrant filled connection.

HRCSA Penetrant inside tubes or enclosed areas.

HRCSA Penetrant can be fogged, or mist applied inside tubes.

Visualization of how the HRCSA Penetrant/Sealer fills the inside of steel tubes when applied with a sprayer fitted with a flexible rust proofing wand with a star tip.

Bearings, Pin Connectors, Interfaced steel

Once all connections are treated properly, the entire steel structure is overcoated with HRCSA self-priming topcoat. Single component, single coat application makes for shortest coating application times in the industry.

HRCSA applied between the bolted in reinforcement plates keep corrosion activity from taking place between the two.

High Pressure Water Cleaning

Posted on

The 5 Energies

The capital spend difference between dry abrasive blast equipment with negative air containment and high pressure water cleaning surface preparation equipment (water recovery and flow-through tarps) can slash your overall surface preparation spend by ~ 50%. Naturally, those costs savings can easily be eaten by labor costs if you do not have the right equipment.

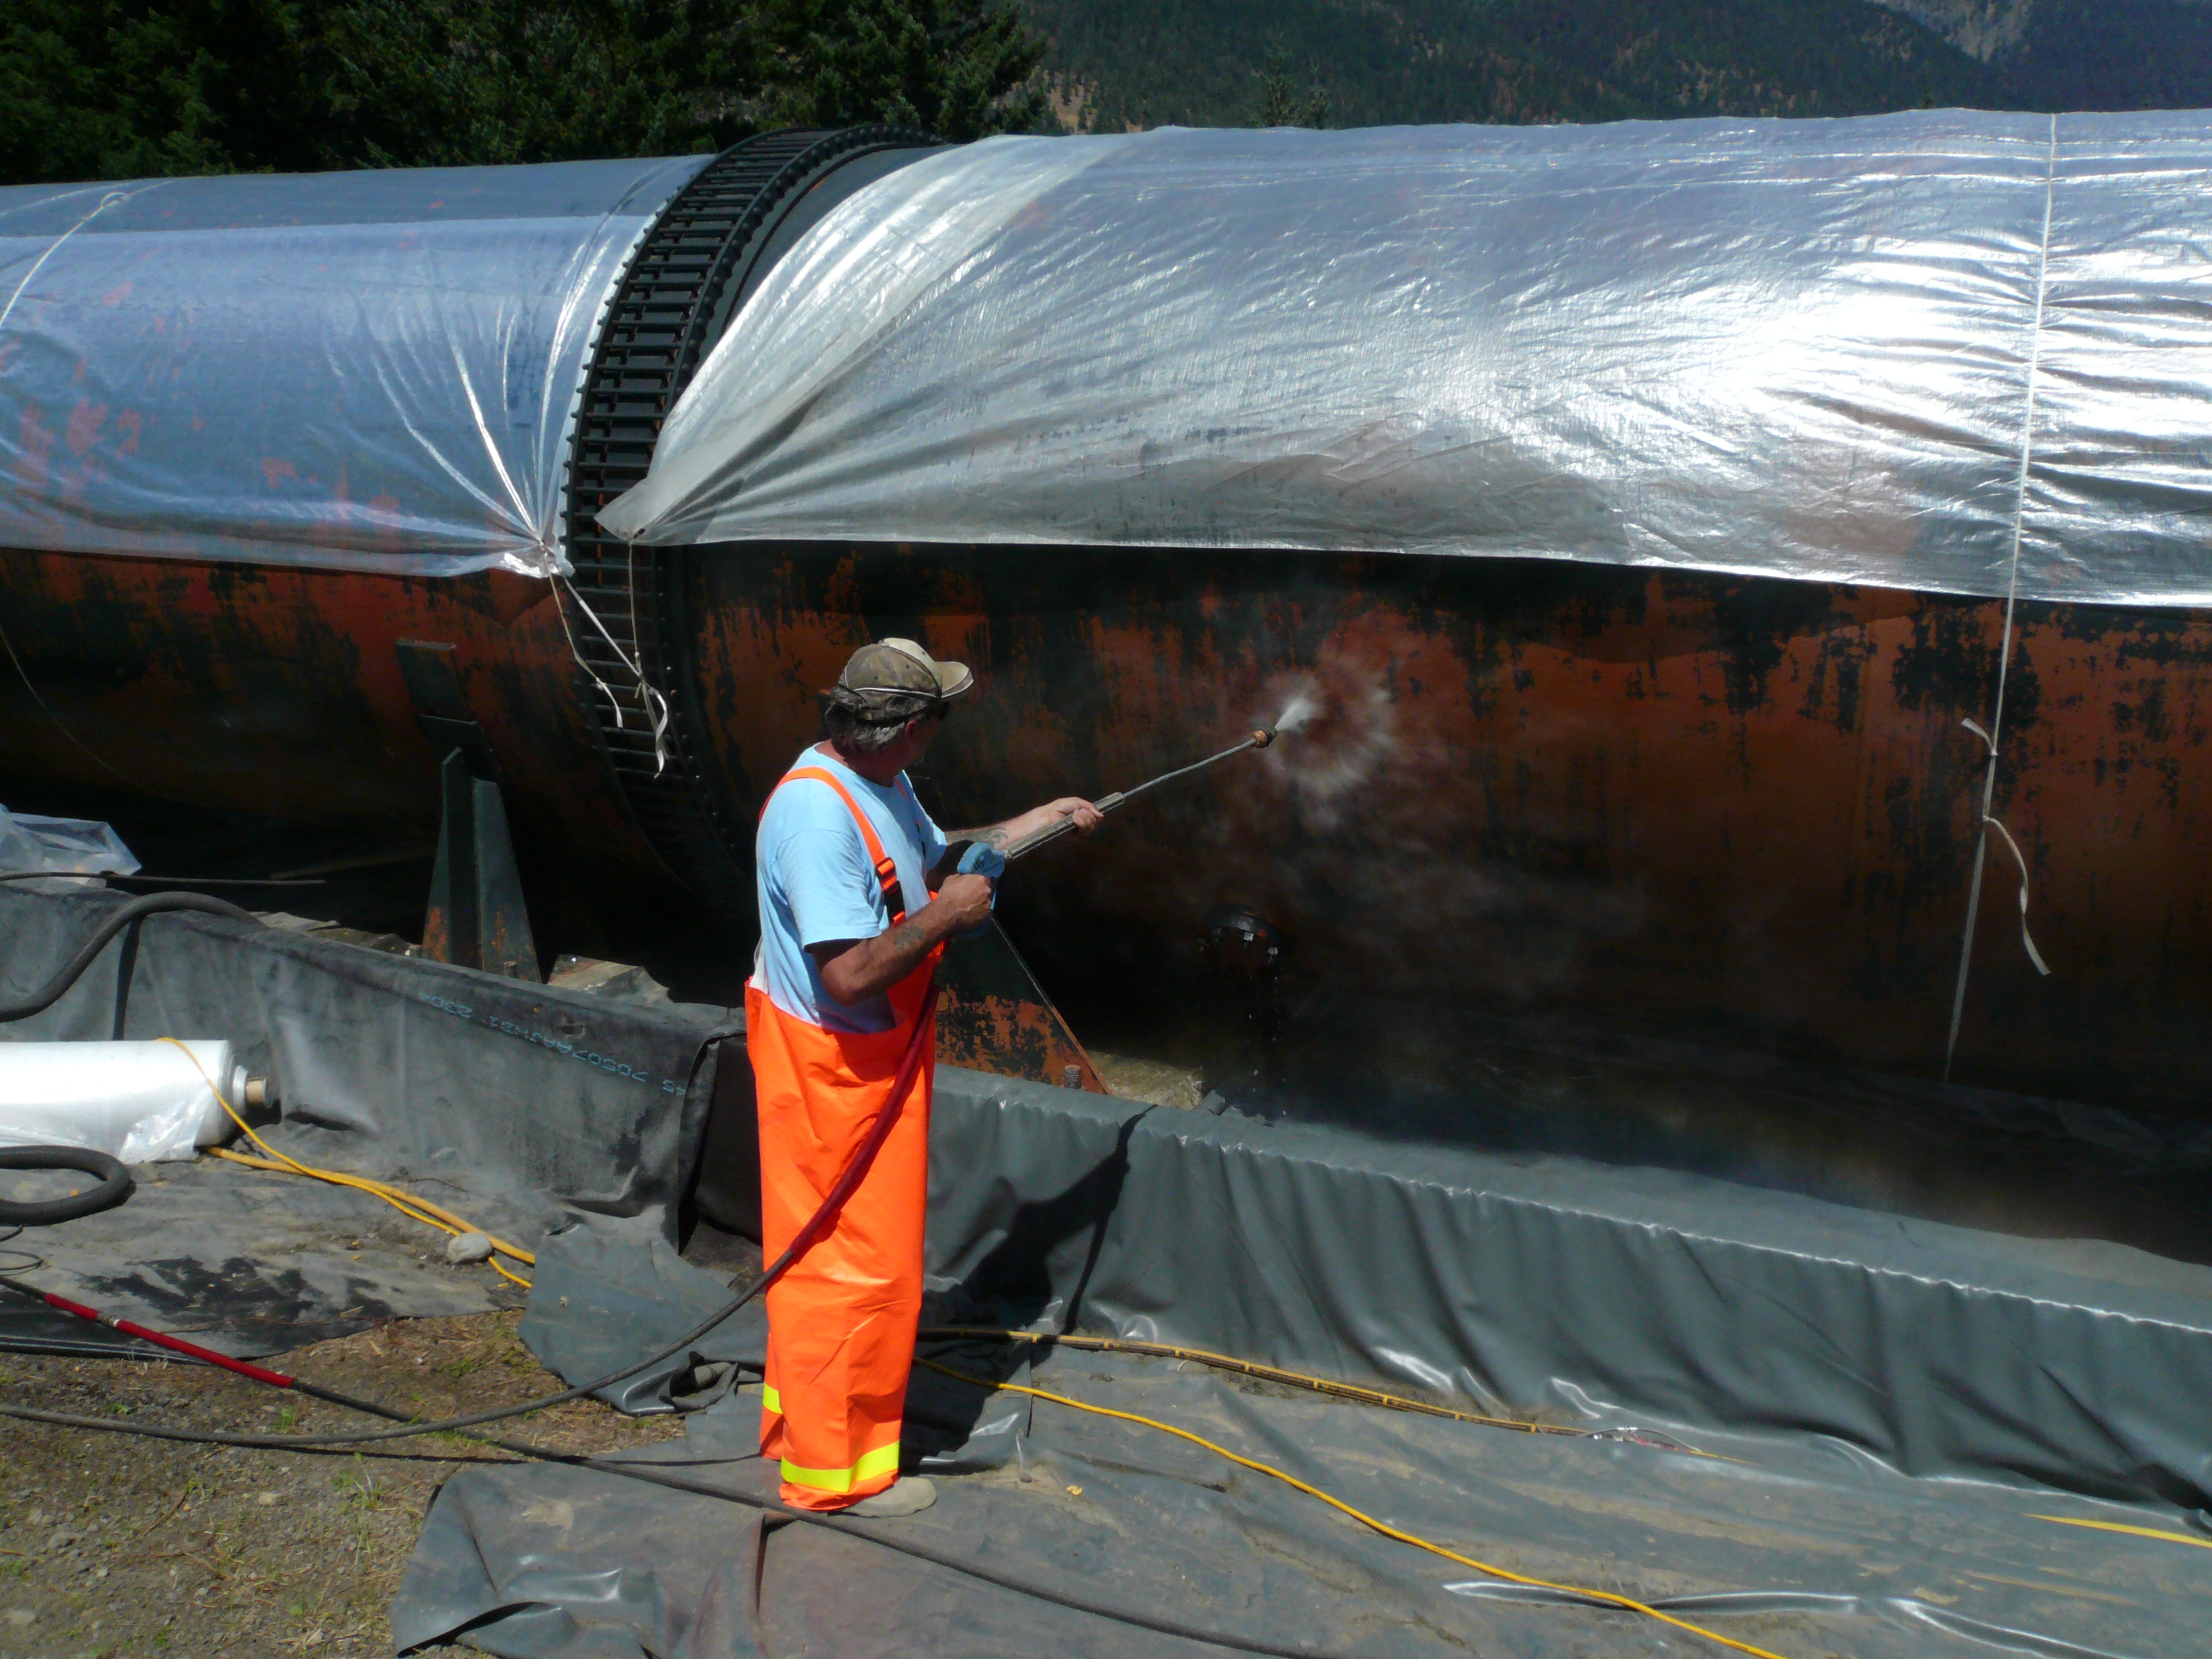
Field experience has shown that 480 bar / 23 lpm hot water (60C) with rotating tip provides the ultimate impact, and balance between effectiveness, efficiency and worker safety.

Pressure & Volume:

When it comes to cleaning, pressure alone is not enough – you also need adequate flow to do an effective cleaning job. The pressure is for cleaning, the volume is for washing.

Field experience suggests that 23 lpm (6gpm) +/- 10%) volume does an excellent washing job and a pressure point of 480 bar (min 350) has produced an adequate cleaned steel substrate for overcoating or recoating with HRCSA.

Heat

Makes removal of salts and contaminants from the surface more effective. Here, field experience has shown that 60C does a superb job at optimizing contaminant removal during cleaning.

AP Chemistry

0 Degree Rotating Tip

Field experience confirms that 0 degree rotating tip “Cutting nozzle” is needed to remove undercutted coating systems, flush out corrosion pits and open up capillary channels inside pack-rust corrosion cells located inside joints and connections.

Salt Remover Additives

Combining the above mentioned forces with a salt removing chemistry provides assurance that

Cleaning Oxidized Coins

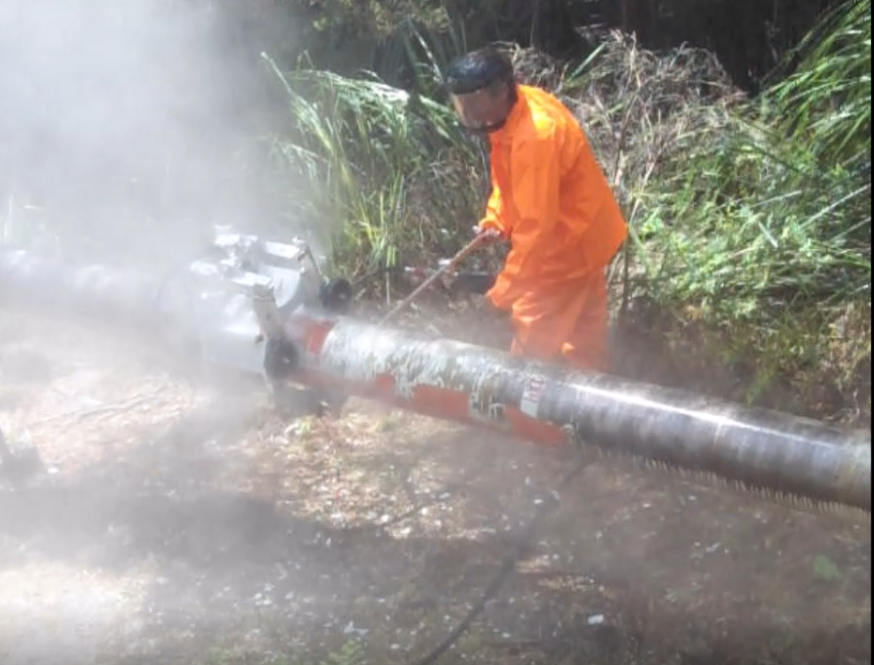
Example of a 480 bar / 23 lpm / hot water with rotating tip cleaning operation at work.

Example of multi-nozzle pressure washing clamp preparing steel for overcoating with HRCSA

Wet Abrasive Blasting

Posted on

Although the vast majority of HRCSA project Surface Preparation is done with High Pressure Water Cleaning and/or hand tool cleaning.

It does happen, on occasion, where abrasive blasting is required (engineer specified, heavy black oxide removal, etc.). Because HRCSA is not profile dependent, the following WAB (Wet Abrasive Blast) configuration using crushed glass has proven quite popular.

Most contractors who work with HRCSA already own 7,000 psi, 6gpm, hot water high pressure water cleaners. They maximize their profits by avoiding the cost of negative air containment [1,000 gallons of fuel / day]. When specifications ask for RECOATING, wet abrasive blasting can be achieved by combining their washers with blasters. Environmentally friendly abrasion can be found with crush glass media.

The magic lies in the quality and design of the injection nozzle used.

Example of WAB (Wet abrasive blasting) using crushed glass media with pressure washer and media injection pot as per above configuration.

Field Application

Field Uses:

  • Sectional coating removal [To remove lead paint in preparation for welding.]
  • Can facilitate the removal of thick black oxides.

Photo: It is critical for black oxides to be removed and to mitigate the heavy concentrations of salts at the exposed steel substrate.

NOTE: Hand tools are also used to remove surface black oxides.

Be sure to remove black oxides at all interfaces.

Pack-rusted Joints: Do not blast.

Do not introduce media injection to the corrosion build between plates. High pressure water clean with salt remover only before drying and treating with HRCSA corrosion mitigation chemistry.

NOTE: The corrosion inside a pack-rusted connections to only be high pressure water cleaned with salt remover (then blown dried with clean, dry, 100 psi air pressure). DO NOT introduce abrasives into the pack rust otherwise you will clog the capillary channels. These must remain open.

Overcoating Steel Structures

Posted on

Different Technologies, Different Outcomes.

Traditional cross-linking overcoating systems adhere by chemical-mechanical reaction which means that THEY shrink more and more over time stressing the existing overcoated substrate paint systems whereas HRCSA does not shrink meaning that HRCSA overcoated substrate paints will not lift away from the steel as time passes on.

HRCSA overcoat systems adhere through polar bonding and are not reliant on chemical nor mechanical reactions for adhesion producing a low surface energy bond without risk of existing coating delamination.

HRCSA Self-priming topcoat.

Because HRCSA is a chemically active, surface tolerant system, it can be applied to any existing tightly adhered cleaned, salt and black oxide free substrate (avoid applying over rubber or uncured tar). In addition, HRCSA can overcoat tightly adhered, contaminant-free existing coating systems.

Due to HRCSA’s low surface energy, the risk of delamination caused by shrinkage from traditional overcoat systems is very low.

During open forum discussions about structure critical corrosion with chief structural engineers at the Federal Highway and with state bridge authorities, the engineers were disapproving of how ineffective painting structures with traditional barrier coating systems is. Especially with regard to particularly stopping rust bleeding at the crevice corroded connections and corrosion-frozen moving parts and long term reliability.

The low surface energy HRCSA self-priming topcoat does not ‘tug and pull’ (long term) existing substrate coatings – a characteristic that is especially important in cold weather conditions.

The chemically active aspect for the HRCSA self-priming topcoat’s cousin (HRCSA active Penetrant) is field proven to stop structure critical corrosion inside complex joints and connections, moving parts and wire rope.

To discuss a specific project you are considering, please register and the manufacturing licensee in your territory will be notified. Thank you.

← Back

Thank you for your response. ✨

Time(required)